 地图 - 热线
15392885678
地图 - 热线
- 服务热线 - 15392885678 15069779222
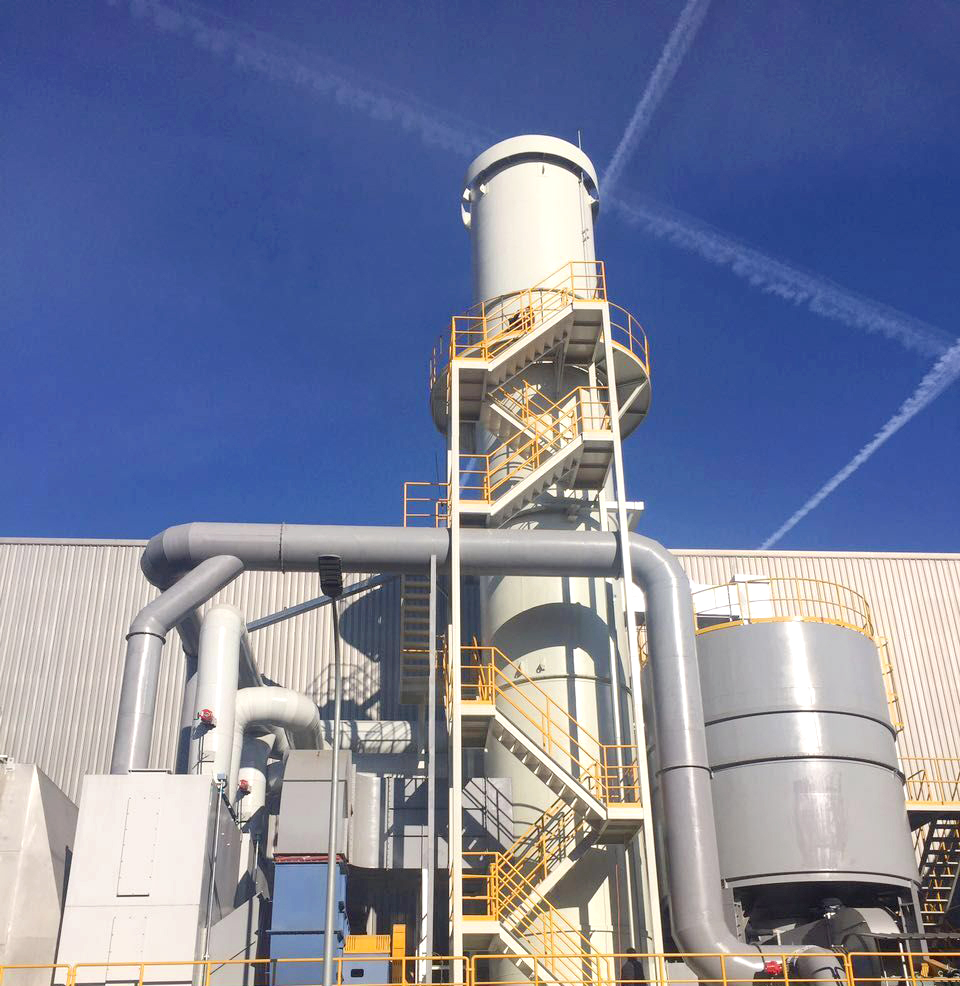
传统VOCs治理工艺长期存在诸多行业短板,活性炭吸附法需要频繁更换耗材,运维成本高且更换下来的废活性炭属于危废,处置流程繁琐、二次污染风险大;单一焚烧工艺针对低浓度大风量废气能耗出众,企业运营压力大;简易喷淋、光氧催化等工艺净化效果有限,难以应对严苛环保抽检,出彩易出现超标问题。沸石转轮+RTO耦合系统针对性破解各类传统弊端,构建快捷、节能、安全、长效的废气治理体系。
Traditional VOCs treatment processes have long had many industry shortcomings. The activated carbon adsorption method requires frequent replacement of consumables with high operation and maintenance costs, and waste activated carbon belongs to hazardous waste with cumbersome disposal processes and high secondary pollution risks. A single incineration process has extremely high energy consumption for low-concentration and large-air-volume waste gas, bringing great operational pressure to enterprises. Simple spray and photo-oxygen catalysis processes have limited purification effects, difficult to cope with strict environmental random inspections and prone to excessive emission problems. The coupled zeolite rotor + RTO system specifically solves various traditional drawbacks and builds an efficient, energy-saving, safe and long-term waste gas treatment system.
在安全性能层面,沸石转轮采用无机分子筛吸附材料,不燃不爆、热稳定性出众,高温脱附过程无自燃风险,有效杜绝活性炭吸附工艺的消防安全隐患。设备采用连续轮转工作模式,吸附、脱附、冷却同步循环进行,可24小时不间断稳定运行,适配工业生产线连续作业需求,不会出现吸附饱和停机、处理中断的问题,保障生产与环保同步推进。
In terms of safety performance, the zeolite rotor adopts inorganic molecular sieve adsorption material, which is non-flammable, non-explosive and highly thermally stable, with no spontaneous combustion risk during high-temperature desorption, completely eliminating the fire safety hidden dangers of the activated carbon adsorption process. Adopting a continuous rotary working mode, the equipment performs synchronous cycles of adsorption, desorption and cooling, enabling 24-hour uninterrupted and stable operation, adapting to the continuous operation needs of industrial production lines without shutdown or treatment interruption caused by adsorption saturation, ensuring synchronous progress of production and environmental protection.
在节能与运维层面,整套系统实现超低能耗长效运行。沸石转轮无需频繁更换耗材,仅需定期清洗维护,使用寿命可达数年,大幅降低耗材与危废处置成本。RTO蓄热循环系统快捷回收余热,大幅降低辅助加热能耗,相比传统直燃设备节能效果显著。同时设备搭载智能控制系统,可根据废气浓度、风量自动调节运行模式,低负荷工况自动节能,进一步压缩运营成本。
In terms of energy saving and operation and maintenance, the whole system realizes long-term operation with ultra-low energy consumption. The zeolite rotor does not require frequent consumable replacement and only needs regular cleaning and maintenance with a service life of several years, greatly reducing consumable and hazardous waste disposal costs. The RTO heat storage cycle system efficiently recovers waste heat and greatly reduces auxiliary heating energy consumption, with remarkable energy-saving effect compared with traditional direct combustion equipment. Meanwhile, equipped with an intelligent control system, the equipment can automatically adjust the operation mode according to waste gas concentration and air volume, and save energy automatically under low-load working conditions, further reducing operating costs.
如今环保监管对VOCs治理的稳定性、安全性、低碳性要求持续提升,沸石转轮+RTO技术凭借全方位优势,有效替代传统低效工艺,成为工业废气标准化治理、企业合规降本、绿色生产升级的优选方案。
Current environmental supervision has continuously improved requirements for the stability, safety and low-carbon performance of VOCs treatment. With all-round advantages, the zeolite rotor + RTO technology completely replaces traditional inefficient processes and becomes the preferred solution for standardized industrial waste gas treatment, enterprise compliance cost reduction and green production upgrading.
地址

服务热线

邮箱

截屏,微信识别二维码